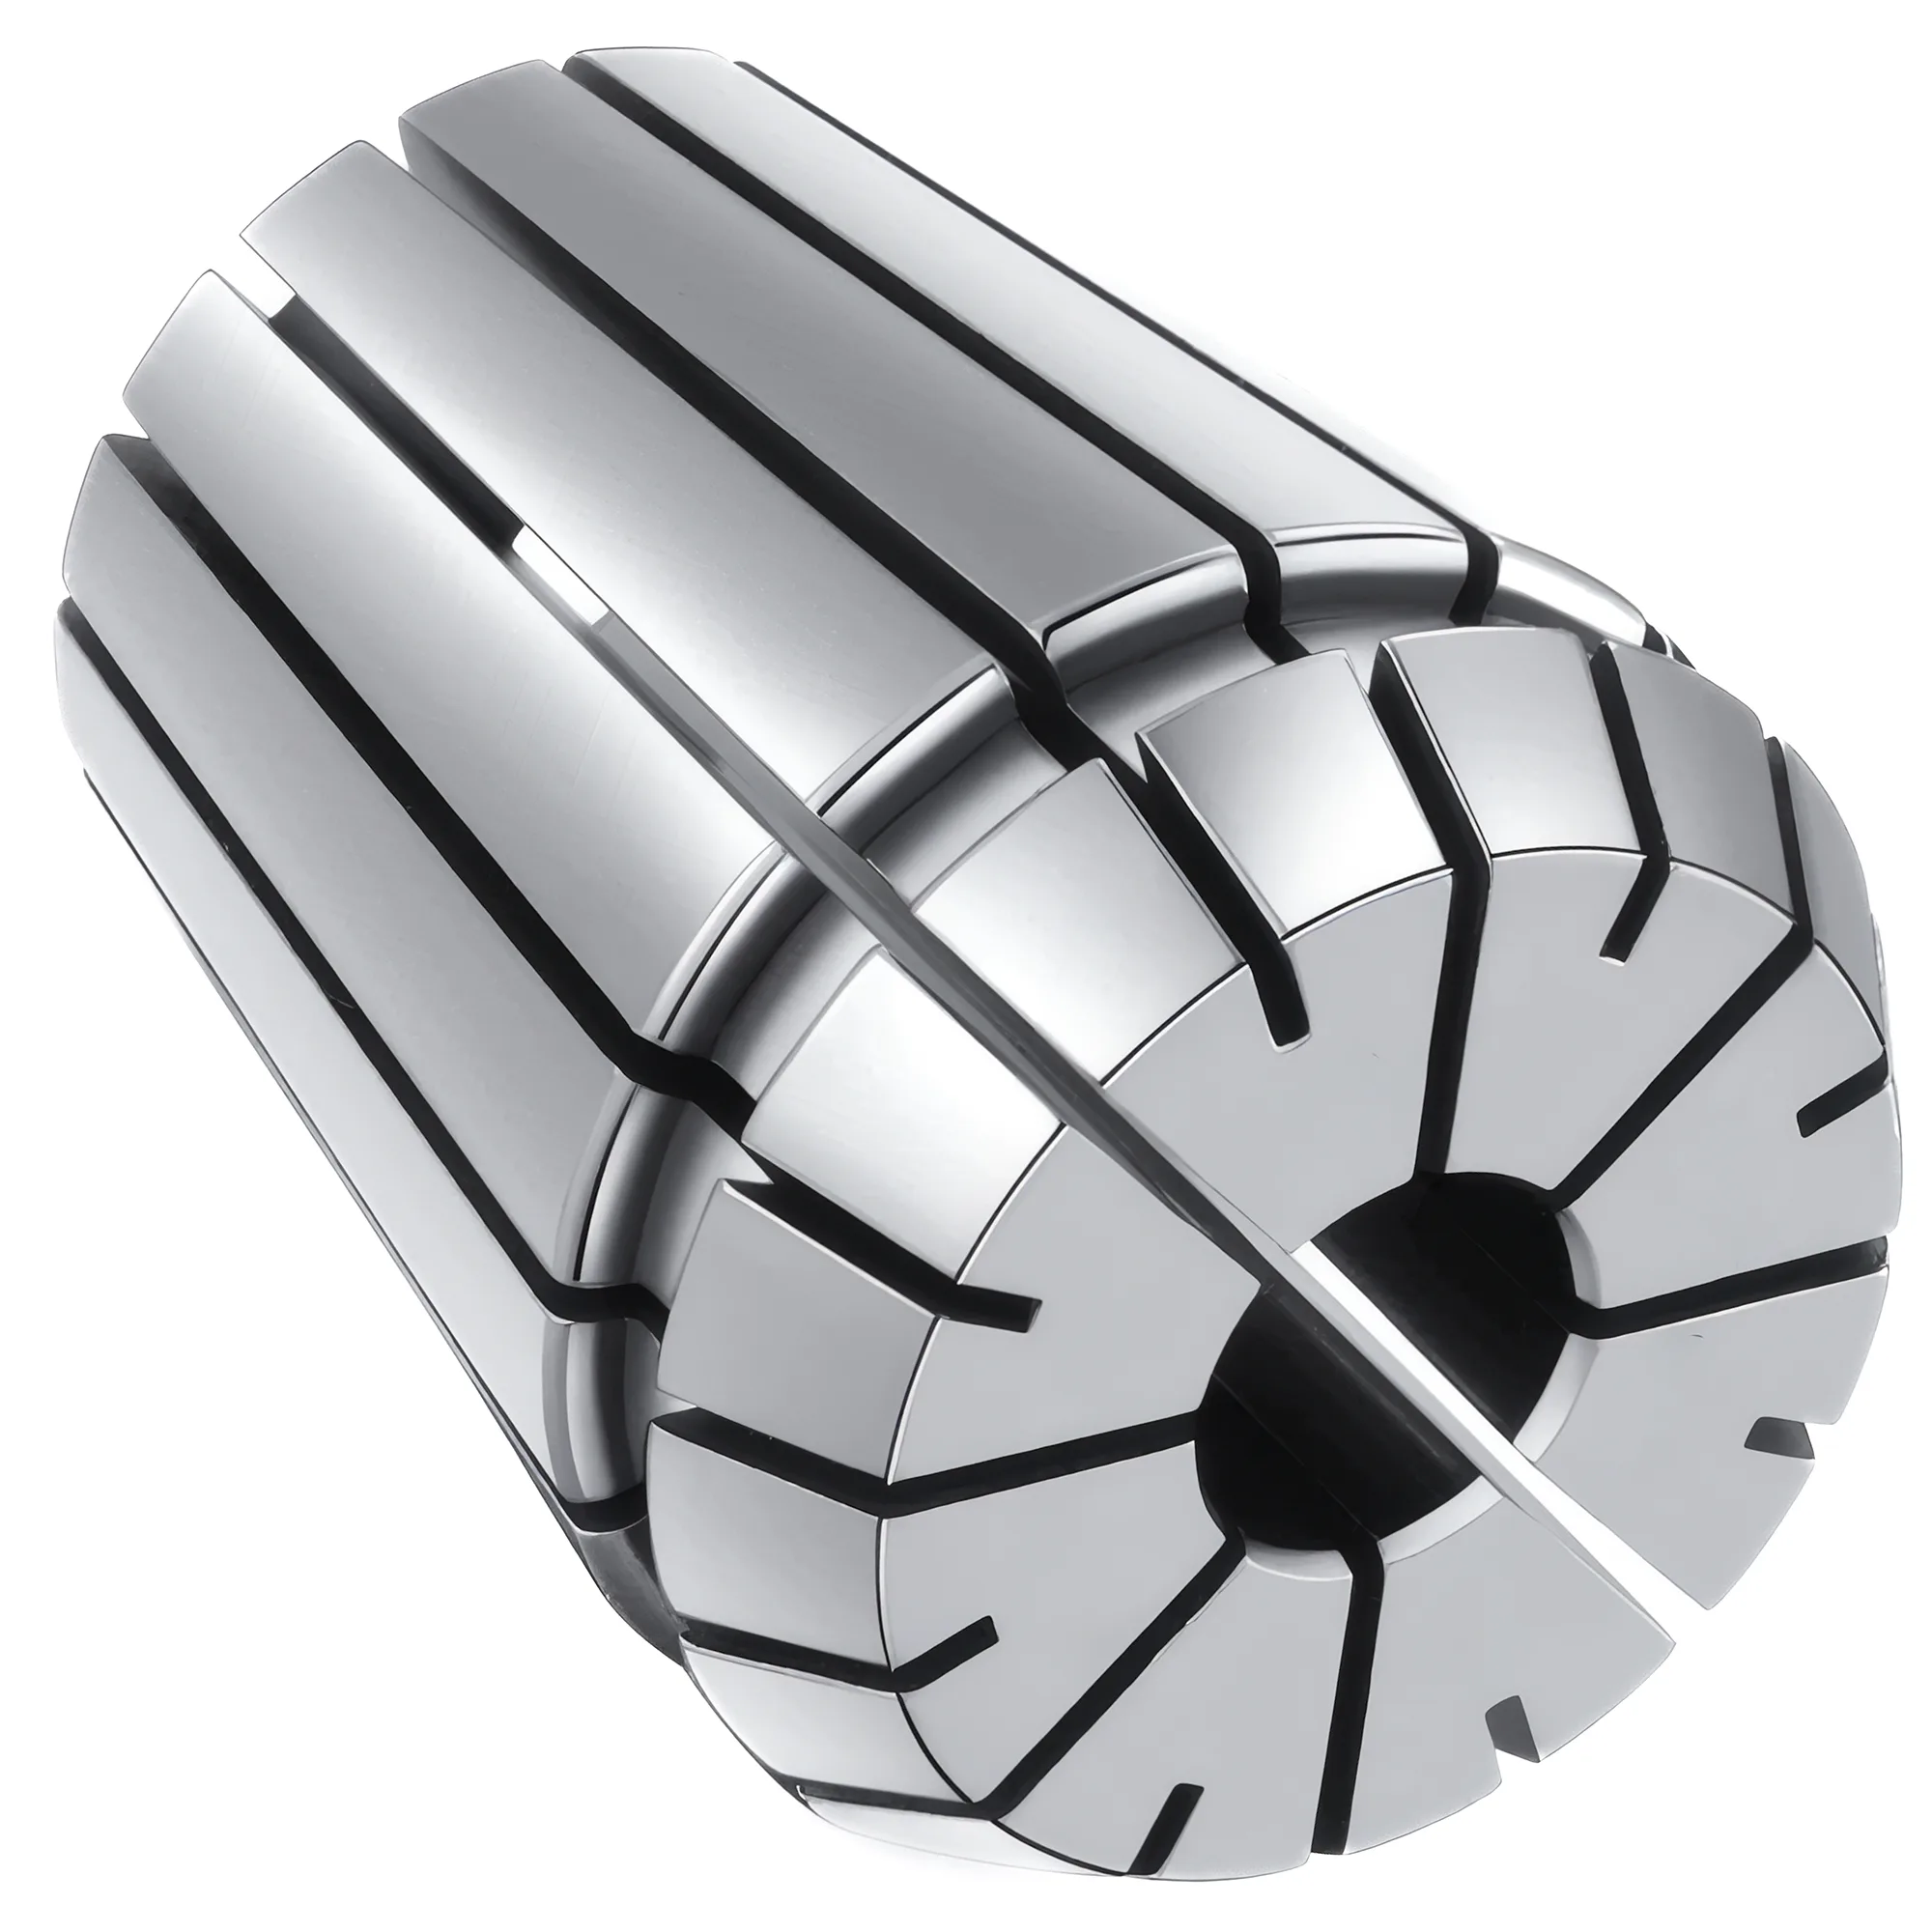
MACHALLY's ER collet range covers eight sizes from ER8 through ER50 — the six ISO 15488 sizes (ER11–ER40) plus ER8 and ER50 — in 303 metric and inch bores clamping 0.5–36 mm and 1/16–1-1/4 in per the published size chart, held to ≤0.005 mm TIR as listed. ISO 15488 (the international form of DIN 6499) fixes the 8° collet setting angle, holder bore and clamping dimensions that make ER collets of the same size interchangeable across holders from any manufacturer. Matching ER nuts and BT, CAT and HSK collet chucks complete the system.
Collet Sizes and Clamping Ranges
The collets are sized by clamping band, not by label: metric sizes step 0.5 mm up to 13 mm and 1 mm above (ER50 steps 1 mm throughout), inch bores about 1/32 in, so the size chart — not the nominal number — shows what fits.
| Series | Metric bores | Inch bores | In ISO 15488? | Typical applications |
|---|---|---|---|---|
| ER8 | 1-5 mm | 1/16-3/16 in | No (manufacturer size) | Micro drills, engraving |
| ER11 | 1-7 mm | 1/16-1/4 in | Yes | Micro-machining, engraving, electronics |
| ER16 | 1-10 mm | 1/16-13/32 in | Yes | Light milling, drilling, small parts |
| ER20 | 1-13 mm | 1/16-1/2 in | Yes | General purpose machining |
| ER25 | 1-16 mm | 3/32-5/8 in | Yes | Medium-duty milling and drilling |
| ER32 | 1-20 mm | 1/16-3/4 in | Yes | General and heavy milling |
| ER40 | 1-26 mm | 1/8-1 in | Yes | Heavy-duty roughing, large drills |
| ER50 | 5-36 mm | 1/2-1-1/4 in | No (manufacturer size) | Large shanks above 26 mm |
ER32 vs ER40 is the usual sizing decision: ER32 tops out at a 20 mm (3/4 in) shank and ER40 at 26 mm (1 in), with ER50 taking over up to 36 mm (1-1/4 in).
For first-time CNC users picking ER sizes against typical end-mill and drill shanks, see the CNC tooling setup beginner guide.
Runout Grades and Materials
ISO 15488 defines two runout classes for ER collets — Class 2 (normal grade, ≤0.015 mm TIR for d₁ ≤ 10 mm and ≤0.020 mm for d₁ 10–26 mm) and Class 1 (≤0.010 / ≤0.015 mm) — and the as-listed ≤0.005 mm collets in this range sit tighter than Class 1, in the band manufacturers usually label UP or AA. A PRECISION grade in 60Si2Mn spring steel at ≤0.003 mm and an ECONOMY grade in 65Mn at ≤0.008 mm are quoted on request; all three grades are hardened to HRC 46-48.
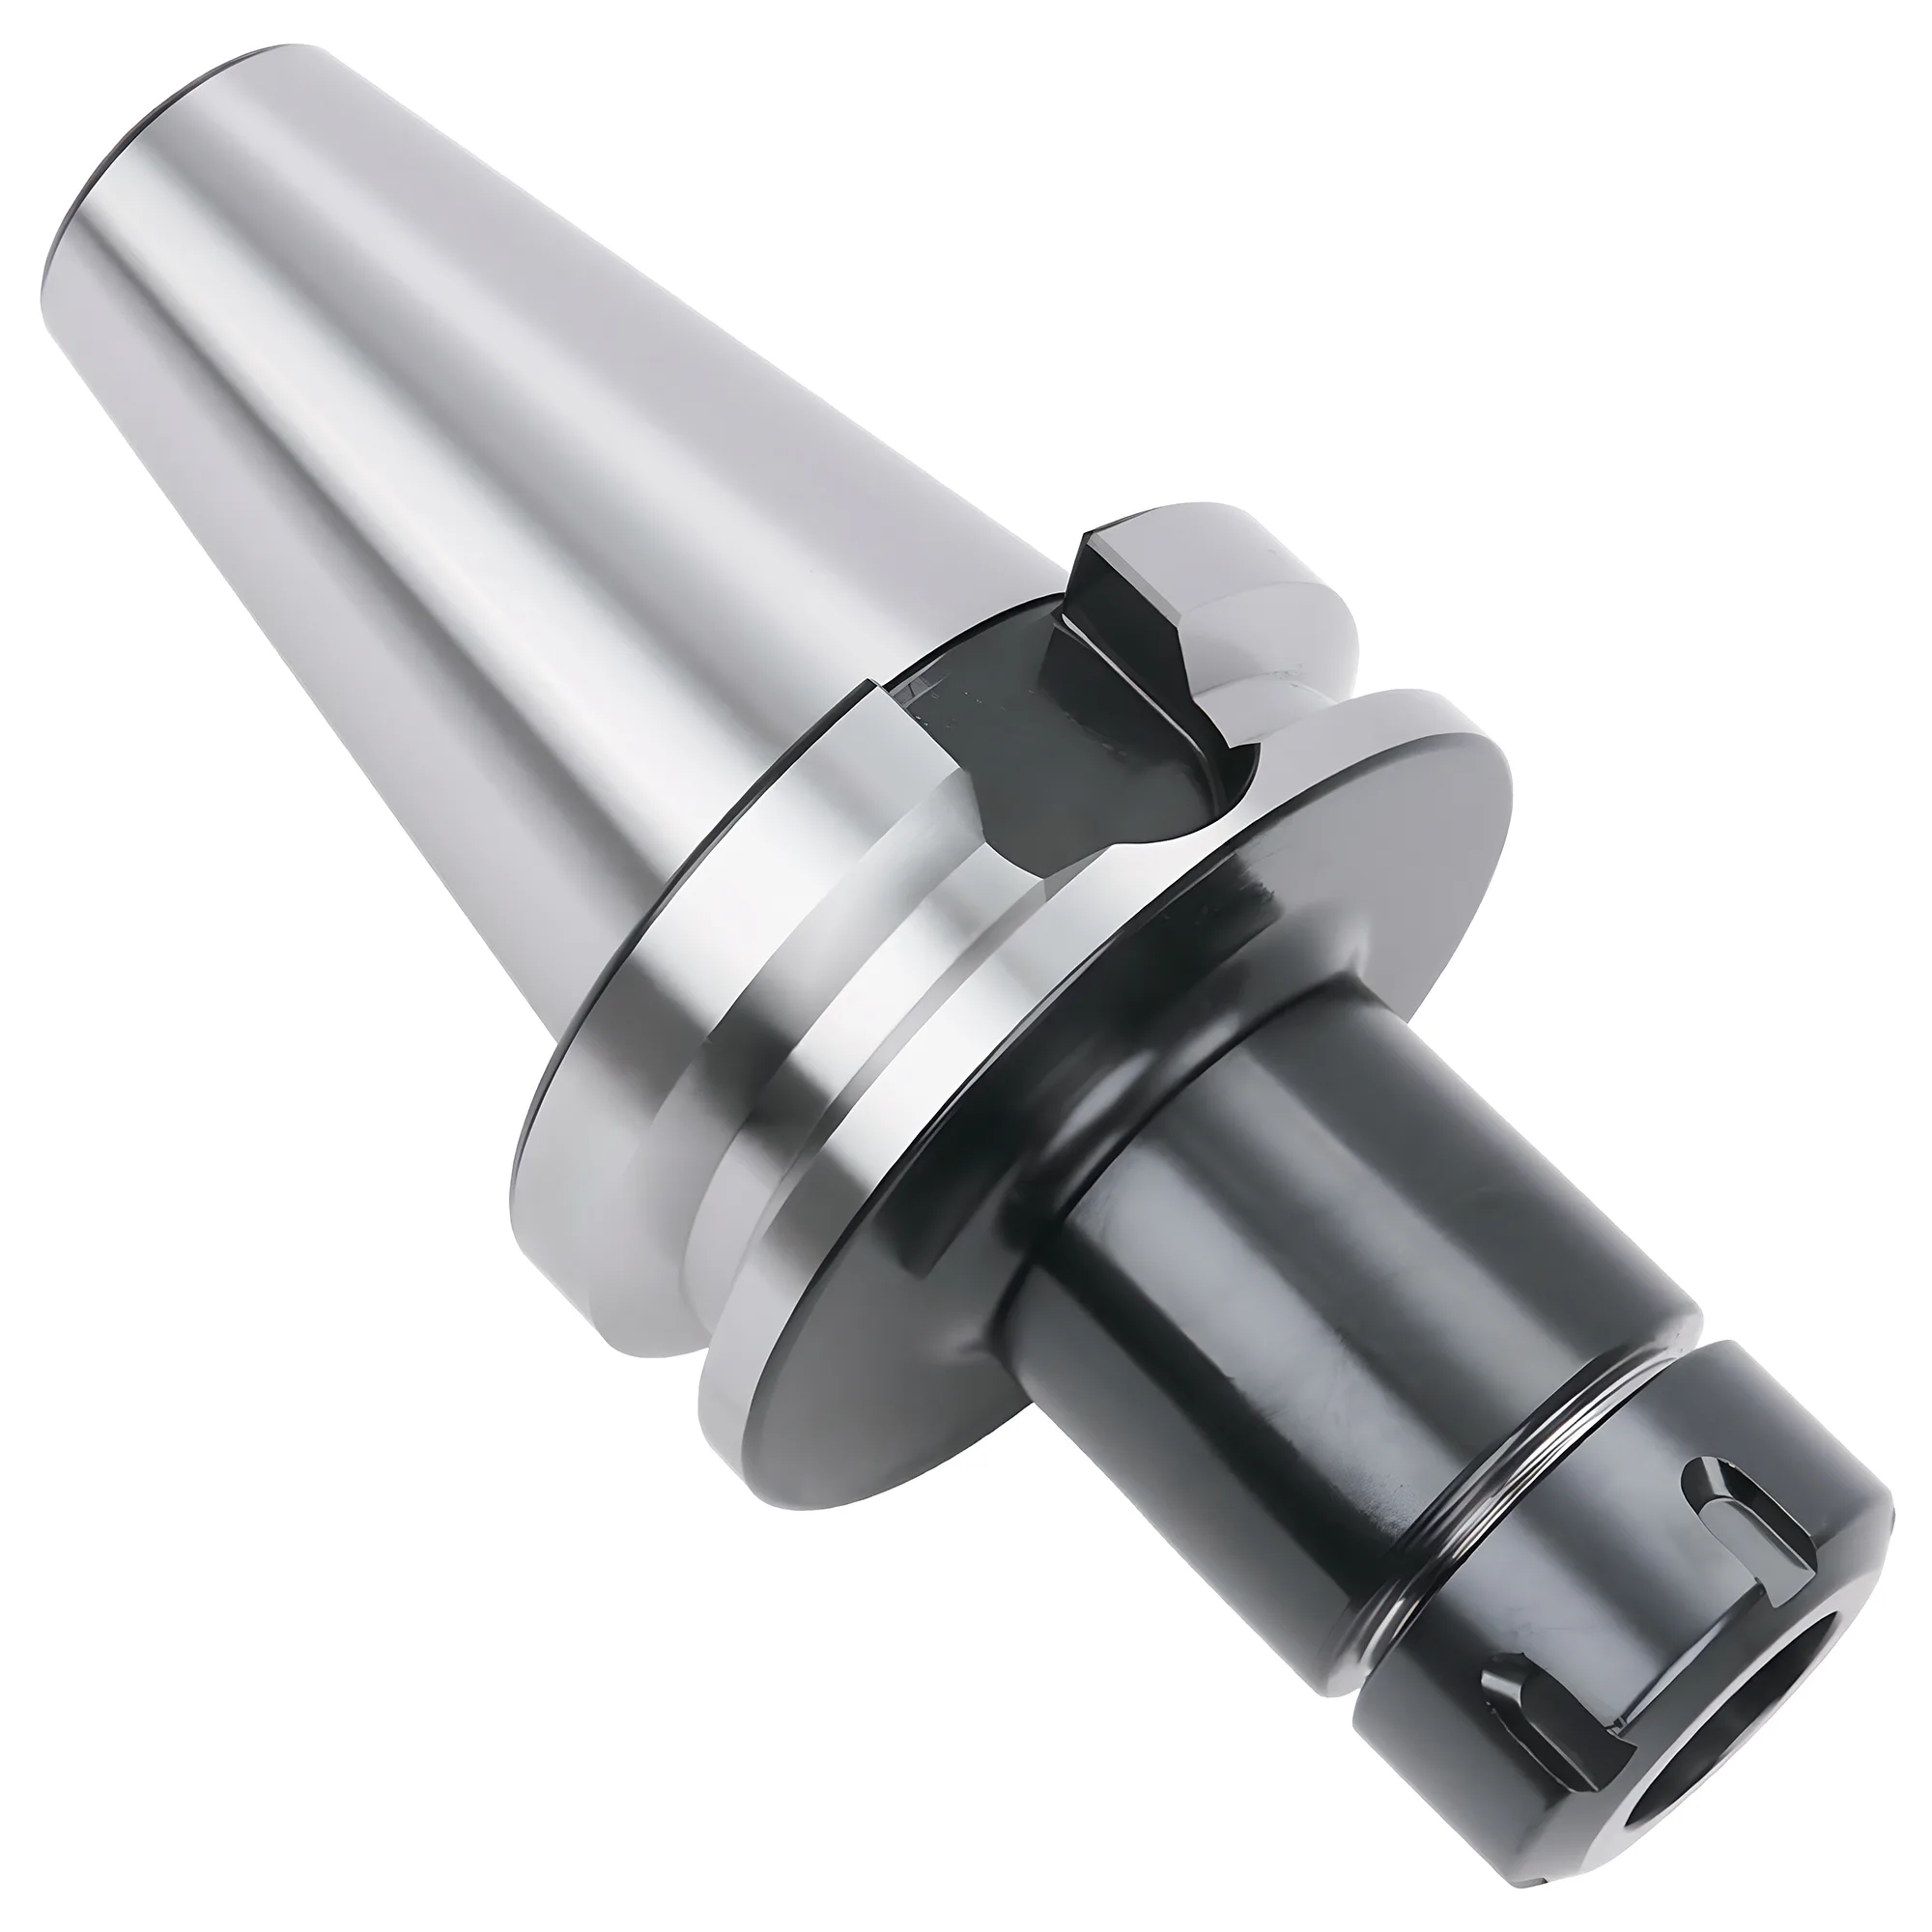
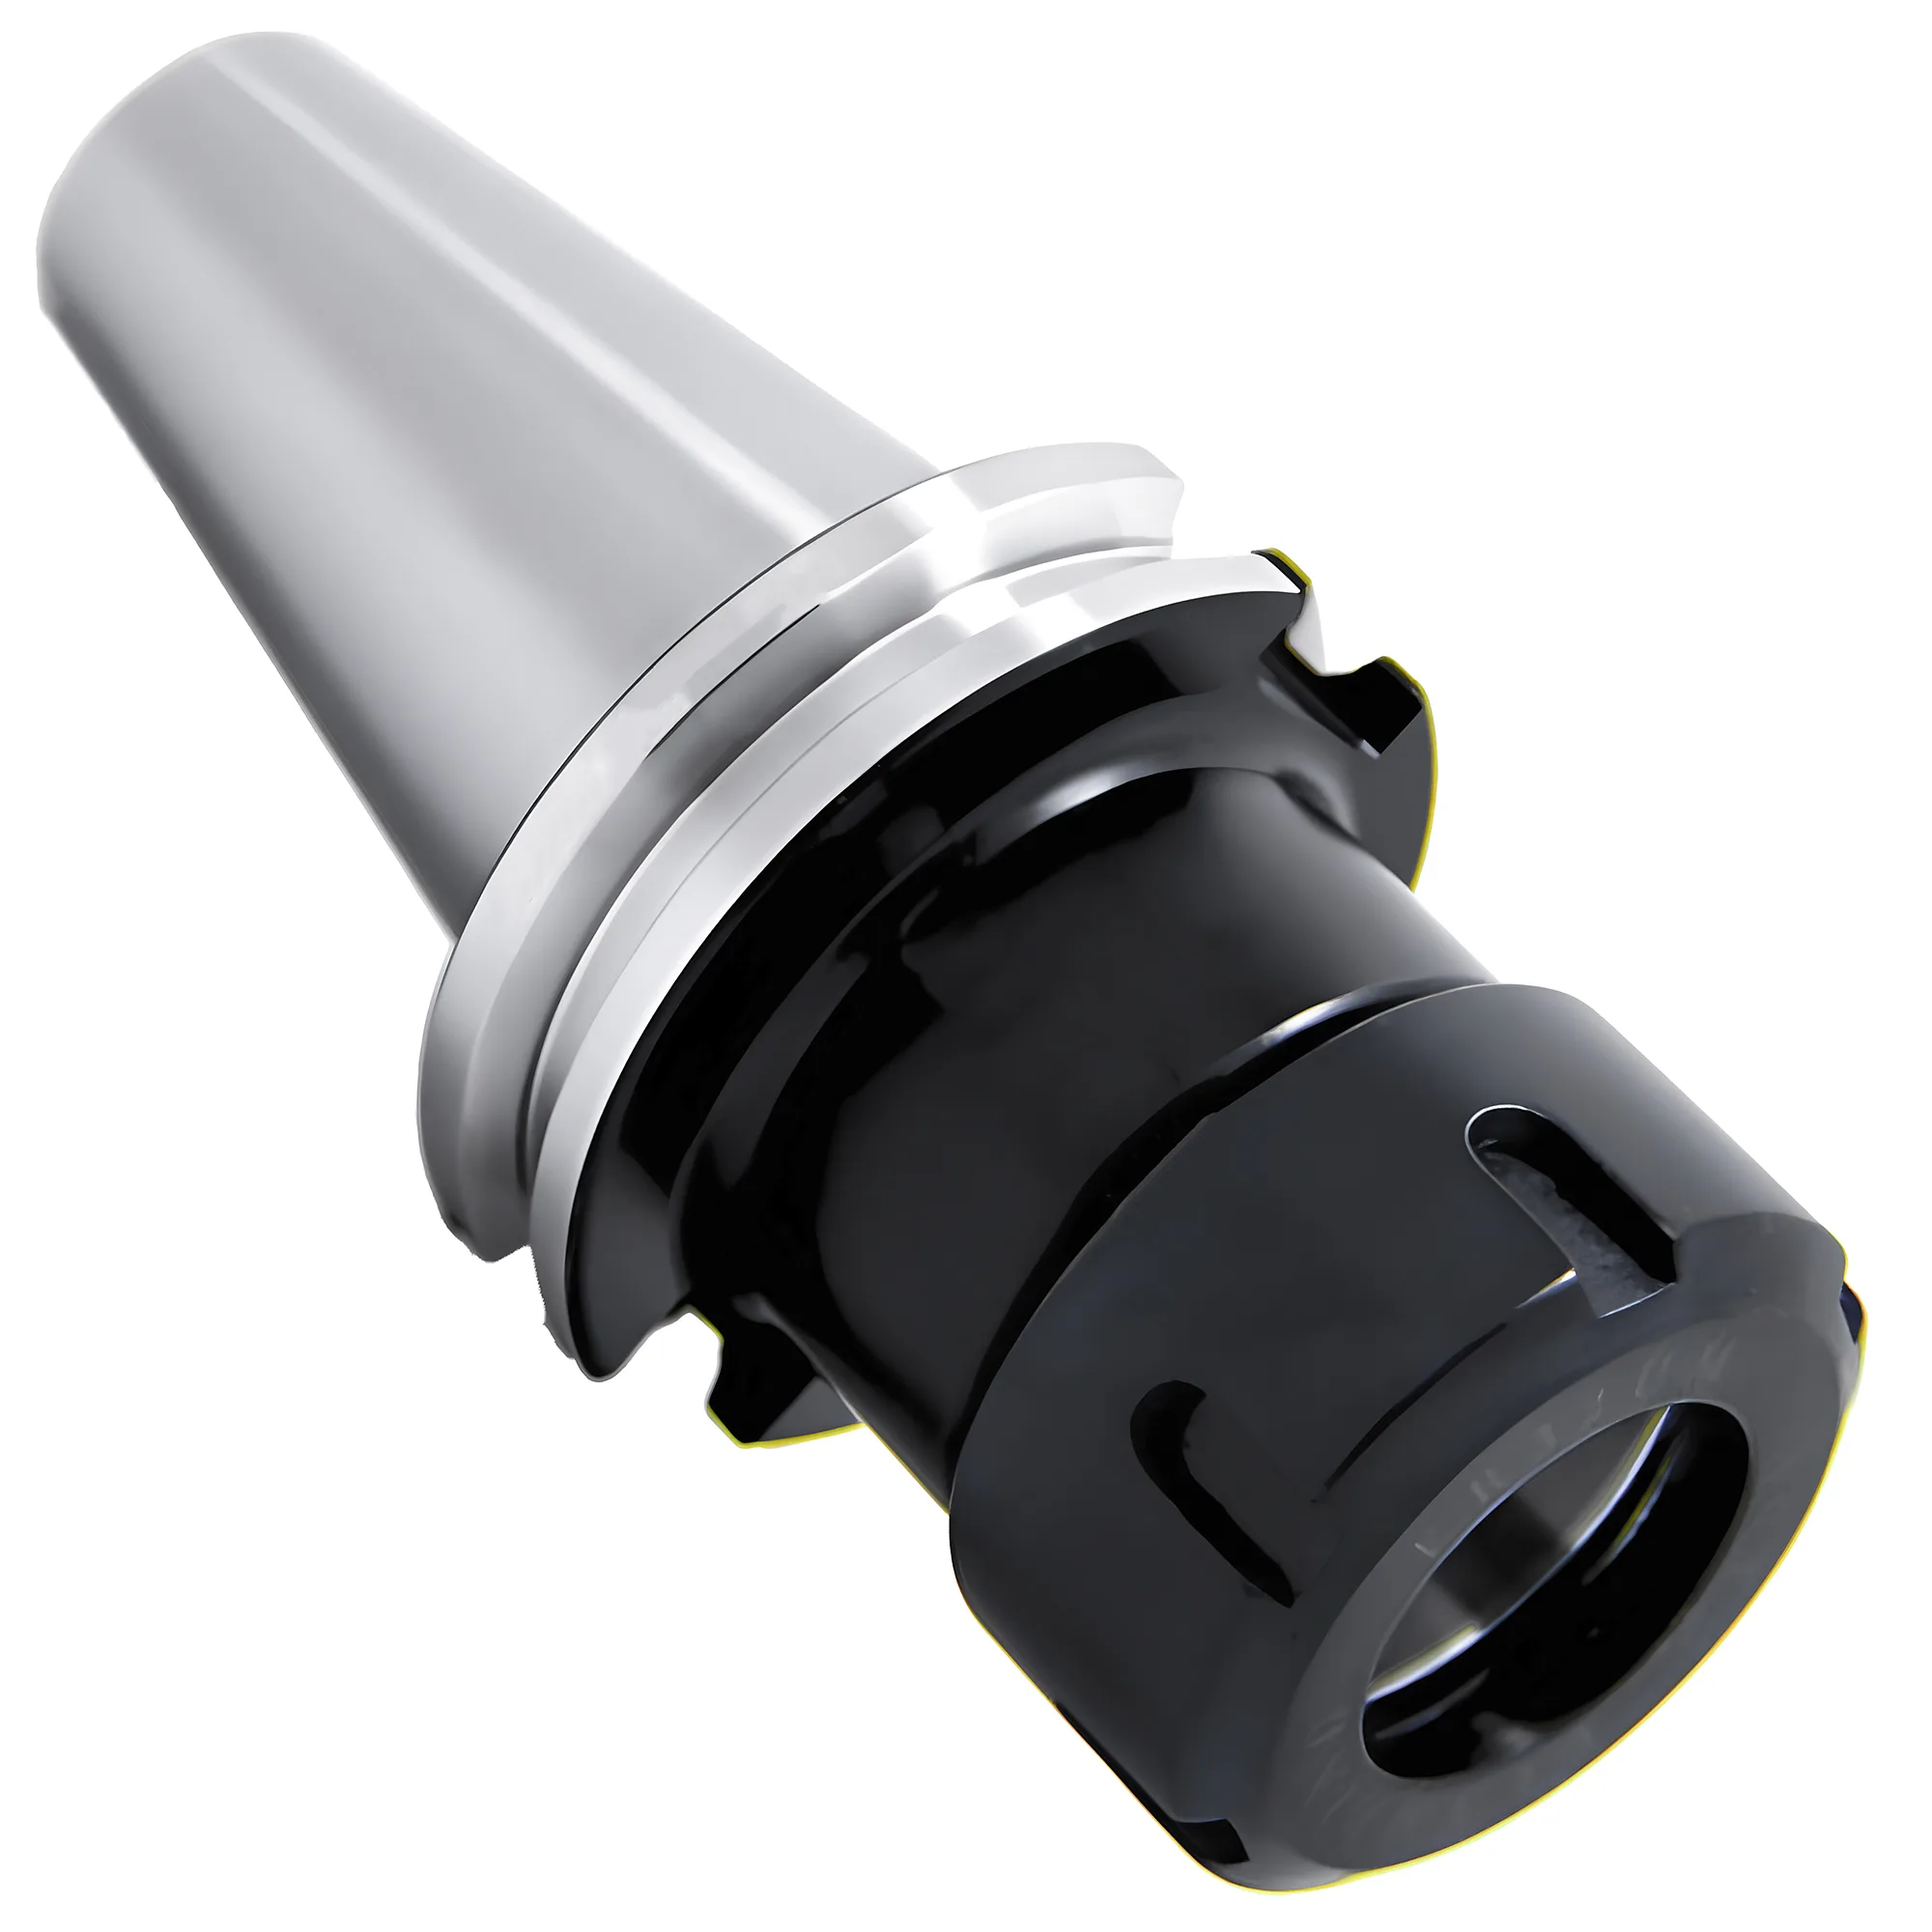
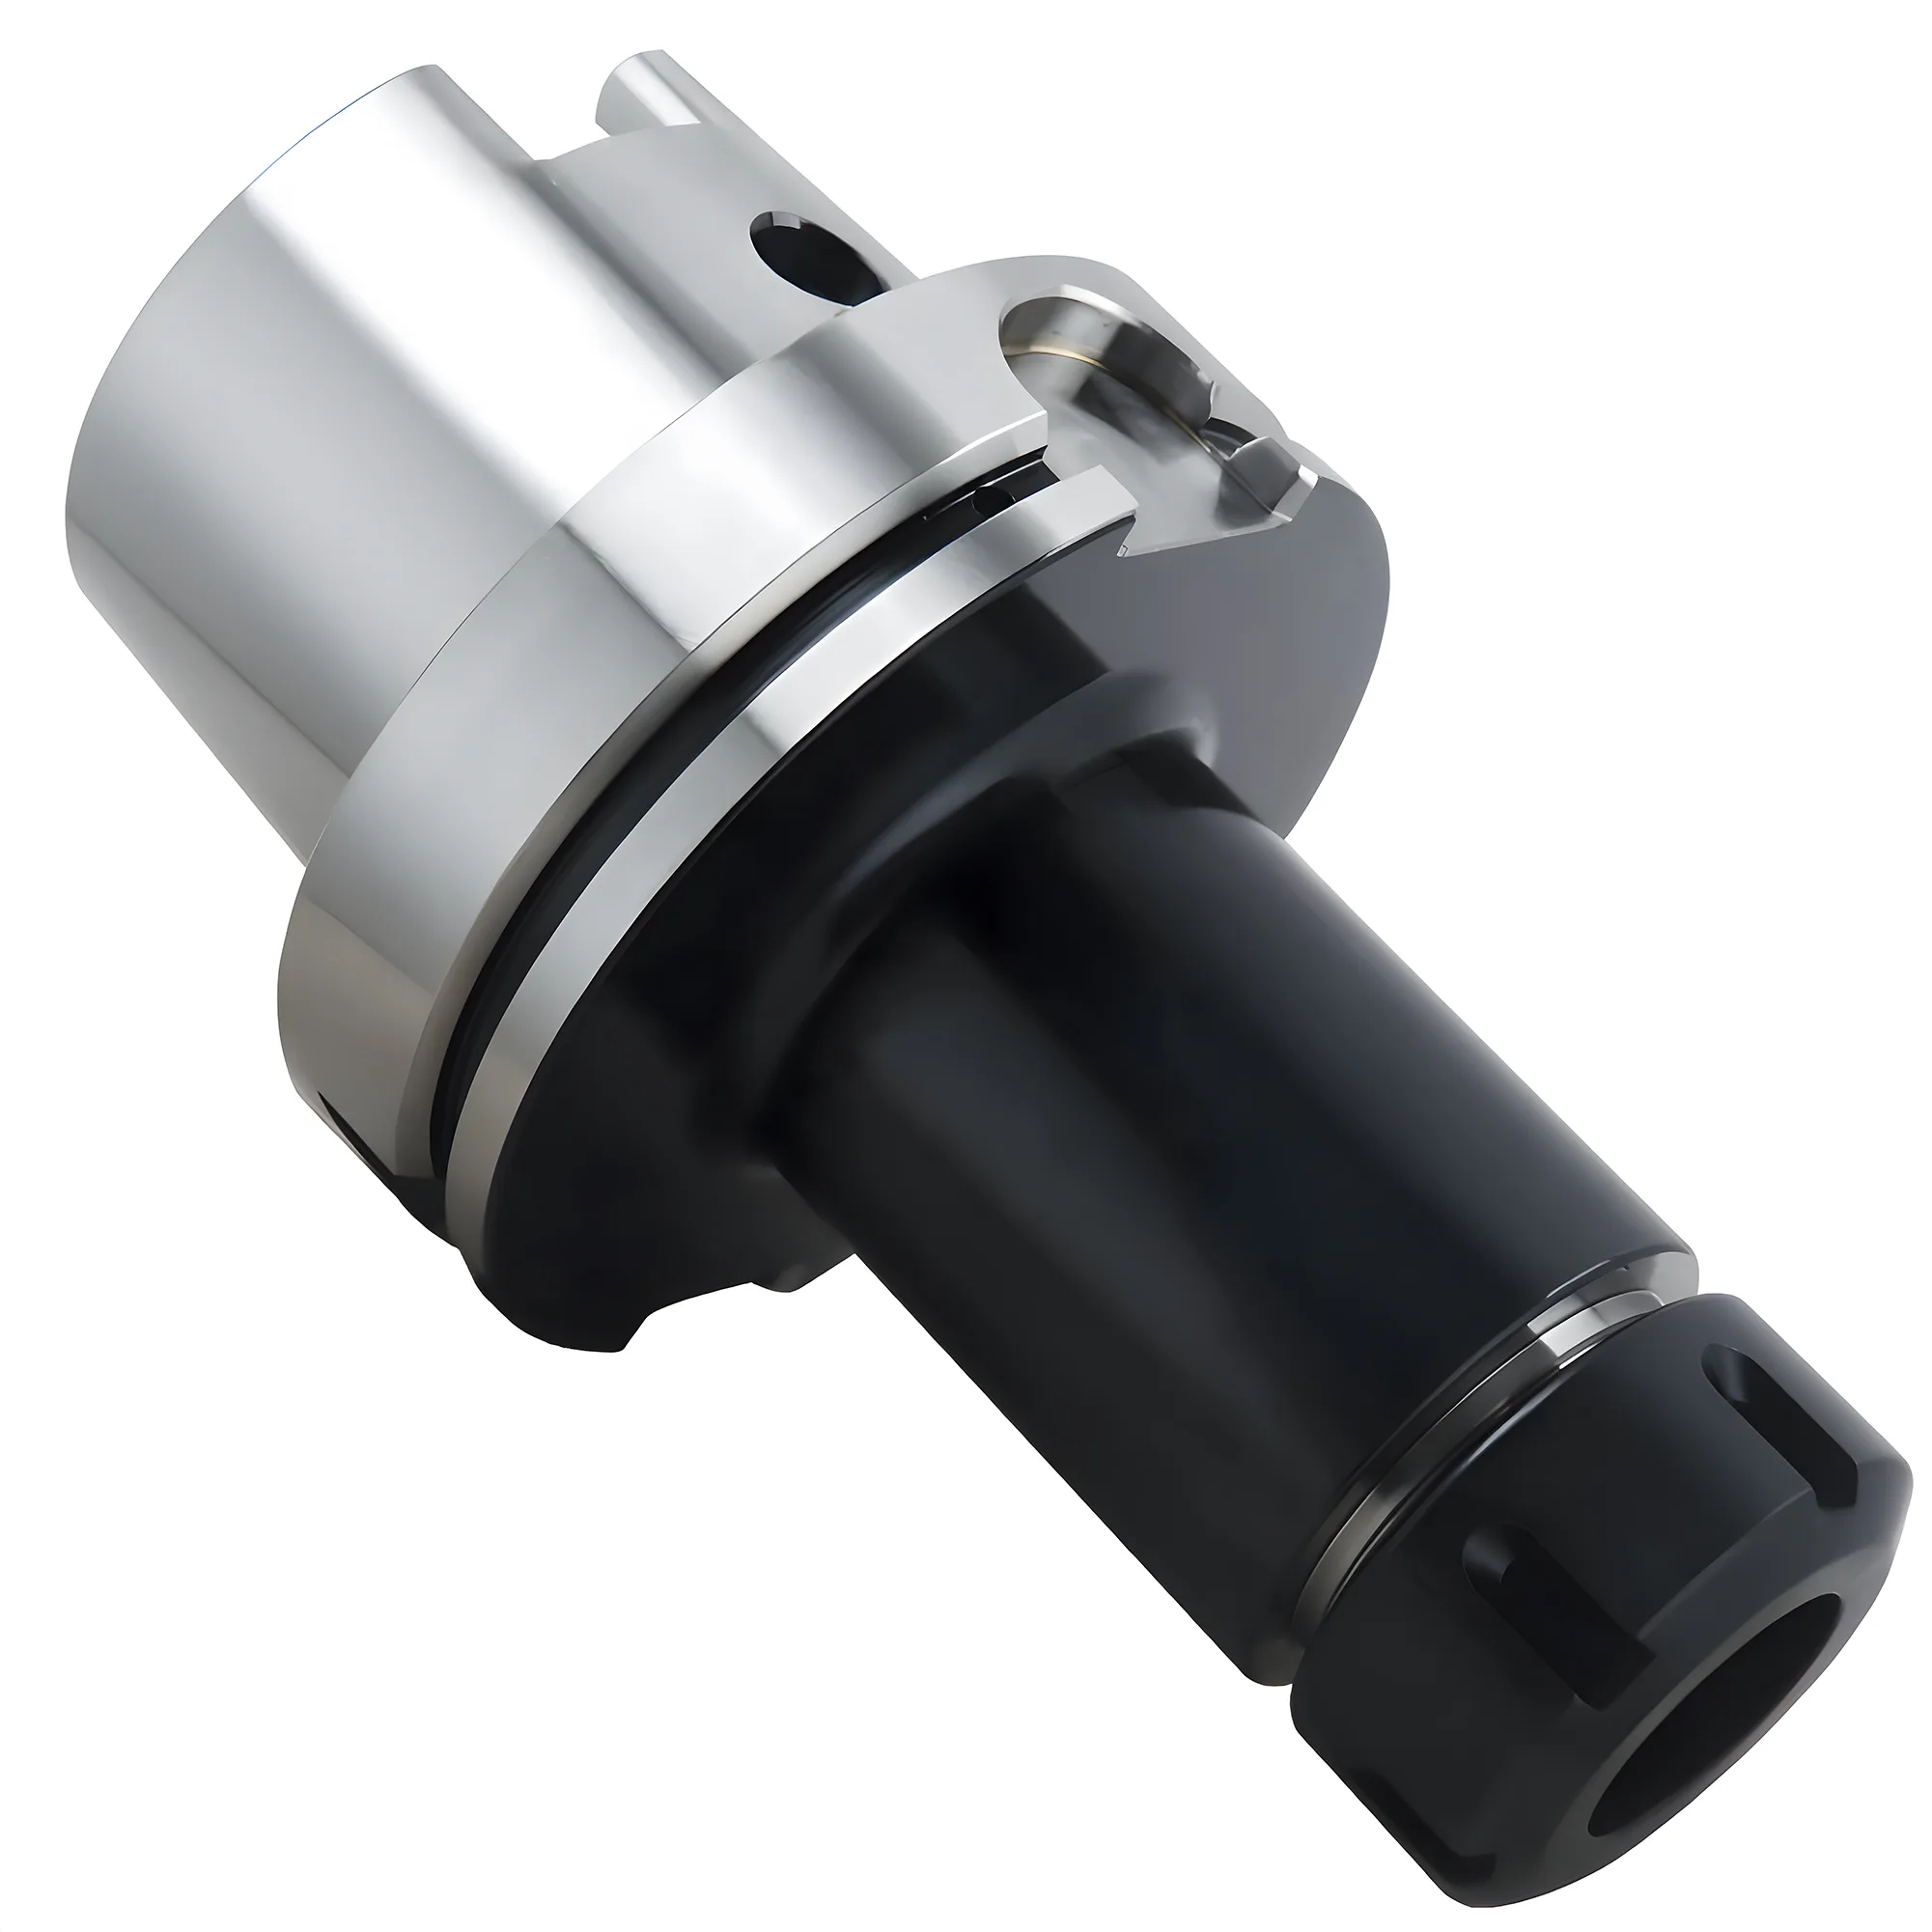
The collet chuck holders are built on BT30/BT40/BT50 (MAS 403), CAT40/CAT50 (ANSI B5.50) and HSK50A/HSK63A/HSK100A (DIN 69893) shanks. BT holders take ER11M through ER50; CAT and HSK holders take ER16 through ER50. Bodies are 20CrMnTi alloy steel vacuum quenched to HRC 56-58 and ground to ≤0.005 mm runout, and any standard ER collet fits.
The shank standard is chosen by the machine, not the collet: MAS 403 fixes the BT taper, ANSI B5.50 the CAT V-flange and DIN 69893 the HSK-A hollow taper, so each holder fits its spindle family while taking the same ER collets.
Nuts, Wrenches and What Ships Together
ER nuts are the one part of the system that is not interchangeable by ER number alone: at the same ER size the nut types do not all share a thread — an ER16 A-type or UM nut is M22×1.5, while ER16 M, MS and GER nuts are M19×1.0 — so a nut has to match the holder, not the collet. The 23 nut part numbers cover ER8 to ER50; A-type stops at ER20, M and MS at ER25, GER at ER32, and ER40/ER50 are UM only.
Matching nut wrenches cover ER8 to ER50 in A, M and UM nut types, with hook spanners for nut diameters 18-110 mm per the wrench size chart. Because A, M and UM nuts of one ER size have different outside diameters, each takes its own wrench.
What is included
Collet chuck holders ship with their nut. Collets, nut wrenches and pull studs are ordered separately, and collets and nuts are also sold on their own as replacement parts.
Applications
Milling -- ER32 and ER40 are used for heavy roughing because their clamping force, typically estimated at 10,000-25,000 N depending on applied torque, handles shanks up to 20 mm and 26 mm without setscrew indentation damage; ER50 collets extend the range to 36 mm, and the BT and HSK holder charts list ER50 at 6–34 mm.
Drilling and Reaming -- ER20 and ER25 cover the majority of hole-making diameters from 1 mm to 16 mm, making them the default starting point for drilling and reaming on general-purpose CNC machining centers. Collet concentricity helps hole straightness and position accuracy.
Small Tools -- ER8 and ER11 hold micro drills and engraving tools down to 1 mm nominal bores, where runout is large relative to tool diameter.
Tool Consolidation -- One collet family across eight sizes, with BT holders taking ER11M–ER50 and CAT and HSK holders ER16–ER50, simplifies inventory for shops running varied work.
For where ER collet chucks fit alongside drill chucks, hydraulic, and shrink-fit holders in a complete system view, see the tool holding complete guide.
Full ER Range Now Available
Eight ER collet sizes (ER8–ER50) in 303 metric and inch bores clamp 0.5–36 mm per the size chart, at ≤0.005 mm TIR as listed, with matching A/M/UM/MS/GER nuts, nut wrenches, and BT (ER11M–ER50), CAT and HSK (ER16–ER50) holders that ship with their nut. Size the collet by clamping band and the nut by the holder's thread.